Molding capacity built for difficult parts
Autronic Plastics (API) runs a modern, climate-controlled molding floor of twenty injection molding machines spanning 55 to 1,200 tons of clamp force. Five machine brands cover the range: tie-bar-less Engel Victory presses for small and medium parts with large molds or robot access, Haitian Zhafir Zeres electric presses and Haitian Jupiter two-platen presses for flexible mid-range and large-part work, Toshiba and Sumitomo production presses, and all-electric Sodick machines in a clean-room cell for tight-tolerance precision components.
Production runs three shifts, 24/5, with weekend capacity available for program ramps. Molds are built and maintained in the tool room down the hall, so a steel change or a repair never has to leave the building.
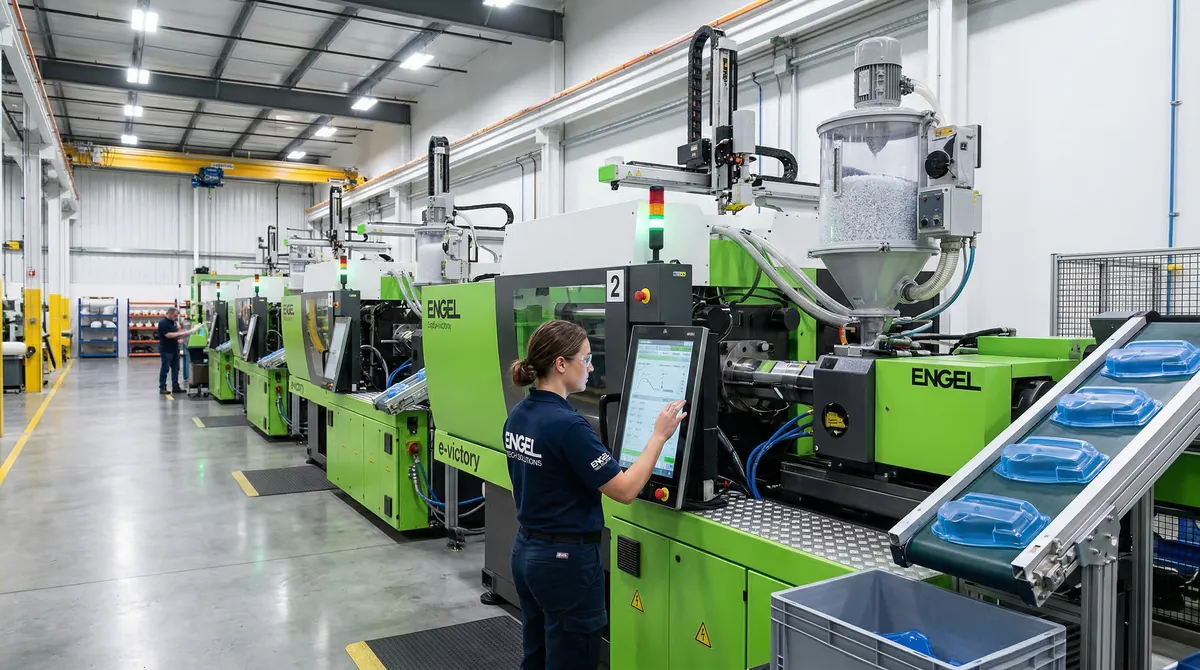
Press list
| Platform | Count | Notes |
|---|---|---|
| Engel Victory (tie-bar-less) | 8 machines | Barrier-free mold area, 130 – 340 T; oversized molds on small presses; fast robot access |
| Haitian Zhafir Zeres (electric) | 3 machines | Electric clamp, injection, and screw drive with integrated servo-hydraulics for core pulls; precise, repeatable, energy-efficient |
| Haitian Jupiter (two-platen) | 2 machines | Servo-hydraulic two-platen clamp for large housings, structural and metal-replacement parts |
| Toshiba | 3 machines | Production molding |
| Sumitomo | 2 machines | Production molding |
| Sodick (all-electric) | 2 machines | Clean-room cell; micro-tolerance precision molding; repeatable shot control |
Twenty presses in total, from 55 to 1,200 tons of clamp force.
Every cell can be fitted with six-axis or top-entry robots for part removal, insert loading, degating, and in-cycle assembly. Central material handling, desiccant drying, and closed-loop mold temperature control keep process windows stable from the first qualified shot to the millionth.
Molding processes
Insert molding
Threaded inserts, bushings, terminals, and stamped or machined metal components are loaded by hand or by robot and over-molded in a single cycle, eliminating a secondary pressing or staking operation. Because API also fabricates metal, the insert and the plastic can be engineered together.
Two-shot and over-molding
Two resins in one process add grip, seals, color breaks, or soft-touch surfaces without assembly. API has established chemical-bond pairings (including TPE and TPU onto rigid substrates) and designs the rotary or transfer tooling that two-shot work requires.
Clean-room precision molding
All-electric Sodick machines in a controlled cell handle small, tight-tolerance components for medical, dental, and electronics programs where contamination control and shot-to-shot repeatability matter more than tonnage.
Engineering and high-performance resins
PEEK, PPS, PEI, PSU, PC, nylons, acetals, high glass-fill compounds, and metal-loaded alloys of up to 94% metal content are routine at API. Our resin guide summarizes the families we run most often. Scientific molding — decoupled fill, pack, and hold with documented process windows — keeps dimensions stable on the materials most shops decline.
Tool transfers
Moving an existing mold to API is a managed process, not a leap of faith. Our engineers review the tool design and condition up front, flag compatibility or quality concerns, and recommend fixes before the first sample. The tool room can repair, re-texture, or re-engineer a transferred tool, and the mold is then qualified, documented, and scheduled so there is no gap in your supply.
- Tool condition and design review before the move
- Repairs, hot-runner service, and steel-safe changes in-house
- First-article inspection and documented process setup
- On-site mold storage and preventive maintenance for the life of the tool
Quality in the cycle, not after it
API is ISO 9001 Certified and a UL Certified molder and assembler. Process parameters are validated and recorded for each tool; CMM, optical, and functional inspection follow the control plan your program requires; and first-article and in-process reports are retained electronically. Read more on our quality page.
Who we mold for
API serves OEMs and contract manufacturers in medical and dental, defense and aerospace, lighting and life safety, automotive, security packaging, displays, and industrial and consumer products. Most programs arrive one of three ways: a part another molder could not hold, a new product that needs tooling and production under one roof, or an existing tool that needs a more capable home.
Frequently asked questions
What size parts can Autronic Plastics mold?
With presses from 55 to 1,200 tons, API molds everything from small clean-room precision components to large structural housings. Tie-bar-less Engel presses allow unusually large molds on smaller machines, which widens the range further.
Do you mold engineering resins like PEEK, PPS, and glass-filled nylon?
Yes. High-temperature and high-performance thermoplastics, high glass-fill compounds, and metal-loaded alloys of up to 94% metal content are a core competency, supported by scientific molding and documented process windows.
Can you take over an existing injection mold?
Yes. API reviews the tool design and condition, repairs or modifies it in our own tool room if needed, then qualifies and documents the process so production continues without a gap.
Where is your molding facility?
All molding, mold construction, metal fabrication, assembly, and shipping happen in our 100,000 sq ft headquarters at 1150 Motor Parkway, Central Islip, NY 11722 on Long Island, about six miles from Long Island MacArthur Airport.
Related
Send us the part other molders declined.
Send a model or a sketch — an API engineer will review it and tell you how we would build it.